Engineered Custom Textile Solutions
Explore our high-performance fabric portfolio manufactured with rigorous OEKO-TEX standards, advanced weave density control, and specialized functional finishing.
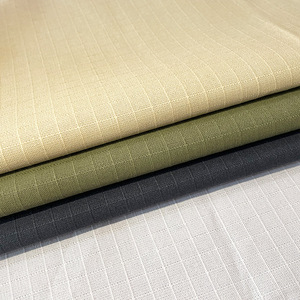
100% Cotton Eco-friendly Ripstop Digital Printed Woven Fabric For Garment Sofas Hats Tablecloths Clothing
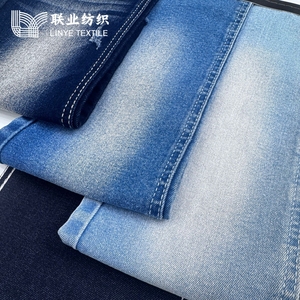
Custom Stretch Denim Fabric Spandex Cotton Blended 9.4oz Soft Woven Material for Pants
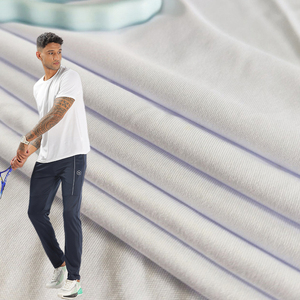
Wholesale 180gsm 180CM Weft 100% Polyester Fabrics For Sublimation Sportswear Soft Quick Dry Anti-Pilling Knit Fabric
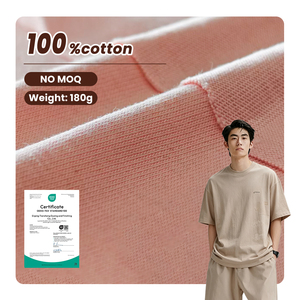
1188 Custom OEM ODM Oeko Certified 100% Cotton Single Side Fabric for High-end All-cotton Tees for Men and Women
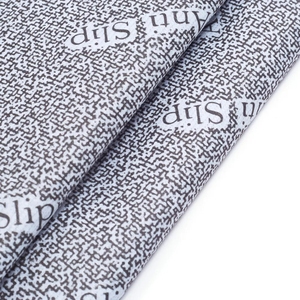
Factory Fashion Printing Polyester Cloth Fabric Mattress Fabric
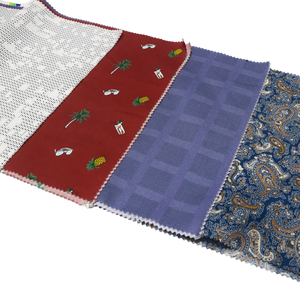
Customized 80%Polyester 20%Cotton 107GSM Lightweight Plain Weave Anti-static Printed TC Fabric for Home Textile
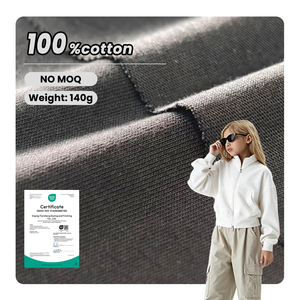
1168 Custom OEM ODM Oeko Certified 100% Cotton Single Side Fabric For High-end All-cotton Tees For Men And Women
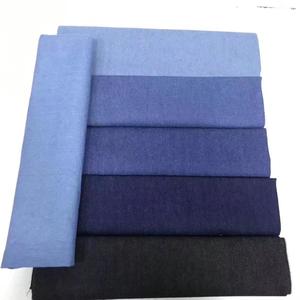
Custom Weight Denim Fabric High Quality Soft Handfeeling for Shirts,dress,suits,blouse,,both Plain or Twill Weave
1. Strategic Overview: Navigating Modern Textile OEM/ODM Manufacturing
In the highly competitive global apparel, home textile, and technical fabric industries, selecting a reliable B2B custom fabric manufacturer is no longer merely a pricing calculation. Today's procurement directors, supply chain VPs, and fashion brand managers face complex challenges ranging from raw fiber volatility and stringent international eco-compliance laws to tight lead times and requests for specialized functional finishes.
As a vertically integrated custom fabric manufacturer and supplier, our mill operates at the intersection of material science engineering and agile textile manufacturing. By maintaining end-to-end operational control—spanning yarn spinning verification, precision warping, circular and shuttle weaving, eco-friendly reactive/dye sublimation printing, to final automated quality inspection—we provide global buyers with verified Information Gain, consistent lot-to-lot color matching, and reliable physical fabric performance.
2. Industry Advantage & Manufacturing Infrastructure
Our manufacturing footprint features state-of-the-art weaving looms, high-speed circular knitting machines, and eco-conscious continuous dyeing and printing lines. We cater to diverse market segments including premium streetwear (heavyweight single jersey cotton), technical workwear (anti-static TC blends), denim apparel (custom-weight stretch denim), sports performance wear (quick-dry moisture-wicking polyester knits), and home furnishings (printed ripstop and mattress tickings).
Vertical Quality Integration
From raw yarn inspection (tensile strength, unevenness U%) to gray fabric weaving and final finishing, every step undergoes strict in-line inspection to guarantee zero defects.
OEKO-TEX & Eco Compliance
All eco-friendly cotton and blended series comply with OEKO-TEX Standard 100 Class I (safe for infants) and REACH regulations, eliminating harmful AZO dyes, formaldehyde, and heavy metals.
Custom OEM/ODM Spec Flexibility
Whether adjusting fabric density (GSM), yarn count (20s to 60s combed), custom width (up to 320cm), or applying functional coatings (water-repellent, anti-static, anti-pilling), we build to exact tech packs.
3. Fabric Material Engineering & Technical Specification Matrix
To assist B2B textile engineers and apparel buyers in identifying the optimal fabric substrate, the following matrix outlines key technical performance parameters across our primary custom fabric product lines:
| Fabric Category | Composition & Blend | Weight (GSM / OZ) | Key Performance Features | Primary B2B Applications |
|---|---|---|---|---|
| Eco Cotton Ripstop | 100% Organic / BCI Cotton | 120 - 240 GSM | Tear-resistant grid, high breathability, reactive print colorfastness (Grade 4+) | Apparel, tactical shirts, outdoor tablecloths, durable hats |
| Custom Stretch Denim | 98% Cotton / 2% Spandex (or Custom) | 4.5 oz - 14 oz (150-475 GSM) | Soft handfeel, dimensional recovery, high tear strength, washing versatile | Fashion denim pants, jackets, skirts, structured suits |
| Quick-Dry Sublimation Knit | 100% Micro-Polyester DTY | 140 - 220 GSM | Moisture-wicking, anti-pilling (Grade 4.5), optimal sublimation ink transfer | Athletic jerseys, activewear, sublimation sportswear |
| Combed Cotton Jersey (1188/1168) | 100% Long-Staple Combed Cotton | 160 - 260 GSM | OEKO-TEX Certified, zero skewness, ultra-soft bio-polished surface | High-end luxury graphic tees, loungewear, designer apparel |
| Anti-Static TC Plain Weave | 80% Polyester / 20% Cotton + Conductive Grid | 107 GSM Lightweight | Electrostatic discharge protection, wrinkle resistance, light breathable | Cleanroom workwear, medical scrubs, protective home textiles |
4. Global Fabric Procurement Trends & Future Market Outlook (2025–2030)
As global trade dynamics evolve, textile procurement strategies are shifting rapidly. Sourcing managers must align with macro trends to ensure sustainable product growth and brand resilience:
A. The Rise of Certified Sustainable & Traceable Raw Fibers
Consumers and regulatory bodies (such as the EU Corporate Sustainability Due Diligence Directive) demand full supply chain transparency. Modern custom fabric suppliers must offer traceable materials including GOTS-certified organic cotton, Recycled Polyester (rPET derived from post-consumer bottles), and Global Recycled Standard (GRS) verified blends without compromising fabric handfeel or durability.
B. Waterless Digital Printing & High-Definition Color Accuracy
Traditional rotary screen printing involves high water consumption and lengthy setup times. Our advanced high-speed digital reactive and dye-sublimation print lines achieve resolutions up to 1200 DPI with minimal water waste. This allows brands to run complex multi-color patterns with lower minimum order quantities (MOQs) and ultra-fast sample prototyping.
C. Smart & Functional Hybrid Textiles
Modern textiles are expected to deliver performance beyond basic aesthetics. The integration of permanent anti-static carbon filaments (as seen in our 107GSM TC fabric), silver-ion antimicrobial finishes, UV-cut protection, and durable water repellency (DWR - C0 eco-friendly chemistry) is expanding from specialized workwear into everyday apparel and home bedding.
5. Step-by-Step OEM/ODM Fabric Sourcing & Quality Verification Roadmap
To minimize commercial risk and guarantee batch consistency, our mill follows an industry-standard 4-phase technical procurement workflow:
Phase 1: Lab Dips & Strike-Offs
Custom color matching via Pantone TCX/TPG references under standard light booths (D65, TL84, CWF). Digital artwork print strike-offs are submitted for customer sign-off within 3–5 business days.
Phase 2: Physical Lab Testing
Sample rolls undergo rigorous physical testing: dimensional stability to washing (AATCC 135), colorfastness to rubbing/crocking (ISO 105-X12), bursting strength for knits, and pilling resistance (Martindale).
Phase 3: Bulk Roll 4-Point System
During mass production, 100% of finished fabric rolls are inspected under the ASTM D5430 Standard 4-Point System. Defect points per 100 square yards are recorded; non-compliant rolls are automatically quarantined.
6. Frequently Asked Questions (FAQ) for Fabric Sourcing Managers
Q1: What are your minimum order quantities (MOQs) for custom fabric development?
Q2: How do you ensure lot-to-lot color consistency across large production orders?
Q3: What certifications do your 100% cotton tee fabrics (1188 & 1168 series) carry?
Q4: Can you engineer anti-static TC fabric for specialized workwear or home textiles?
Q5: What is the lead time from sample approval to bulk container loading?
Partner with a Leading Custom Fabric Manufacturer
Request comprehensive swatch books, lab dip color matchings, or technical spec sheets today. Our fabric engineering team is ready to accelerate your supply chain.
Get Catalog